 EN
 RU
 ES
 FR
 AR
 PT
 IT
 ID
 KO
 TR
 DE
 VN
 TH
 IN
 JA
 ZH
 MS

A printed carton rarely goes to market bare. Before the sheet is cut and creased, most packaging passes through one more station: a thin, biaxially oriented polypropylene film gets bonded over the ink.
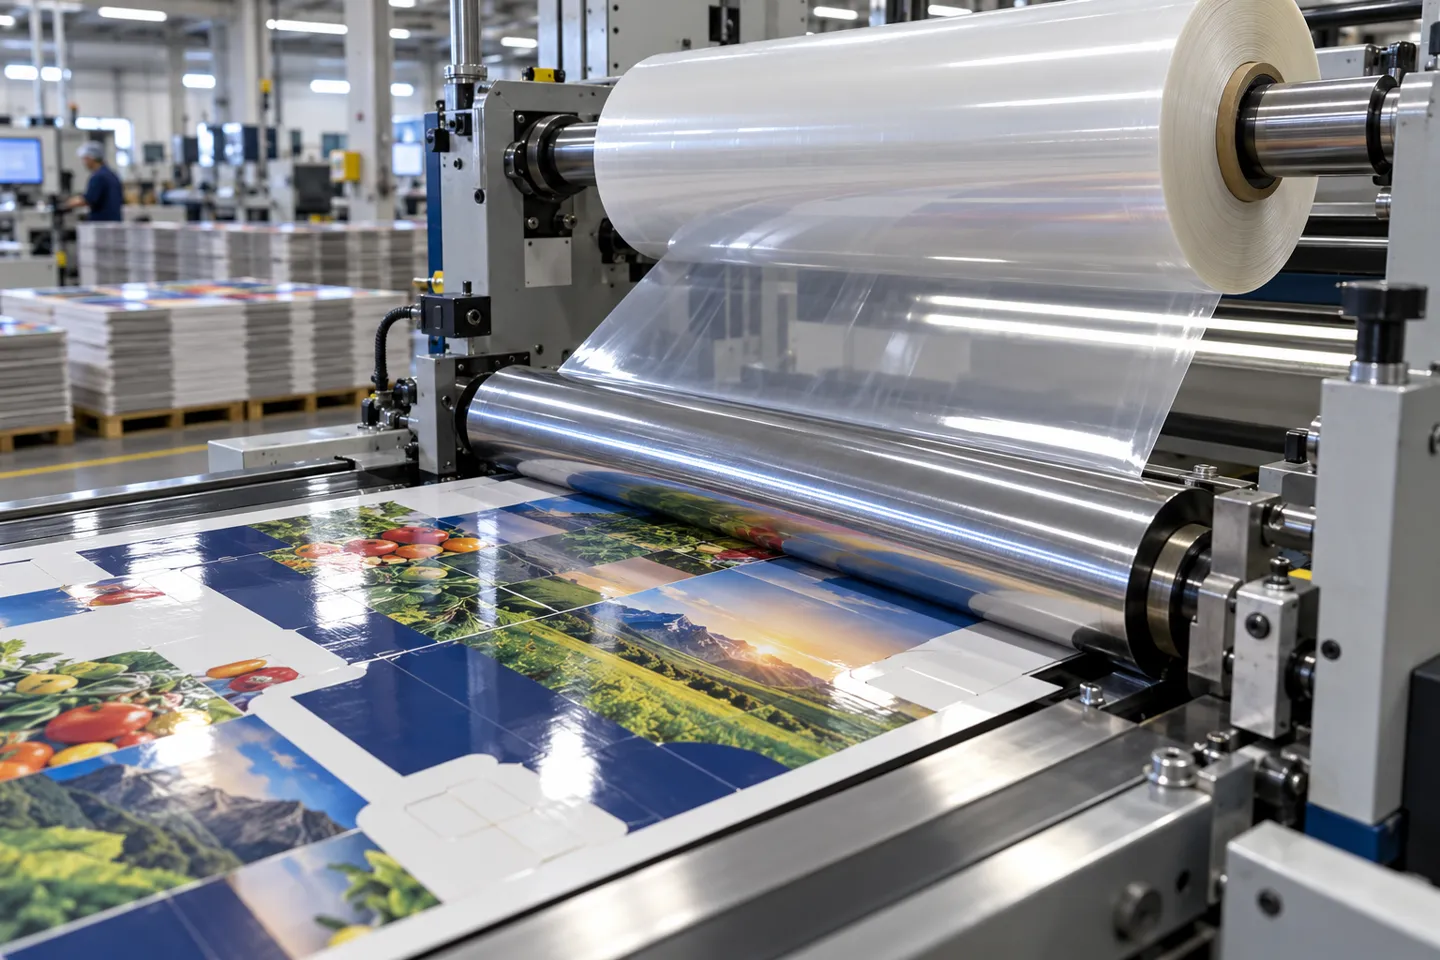
What BOPP Lamination Actually Is
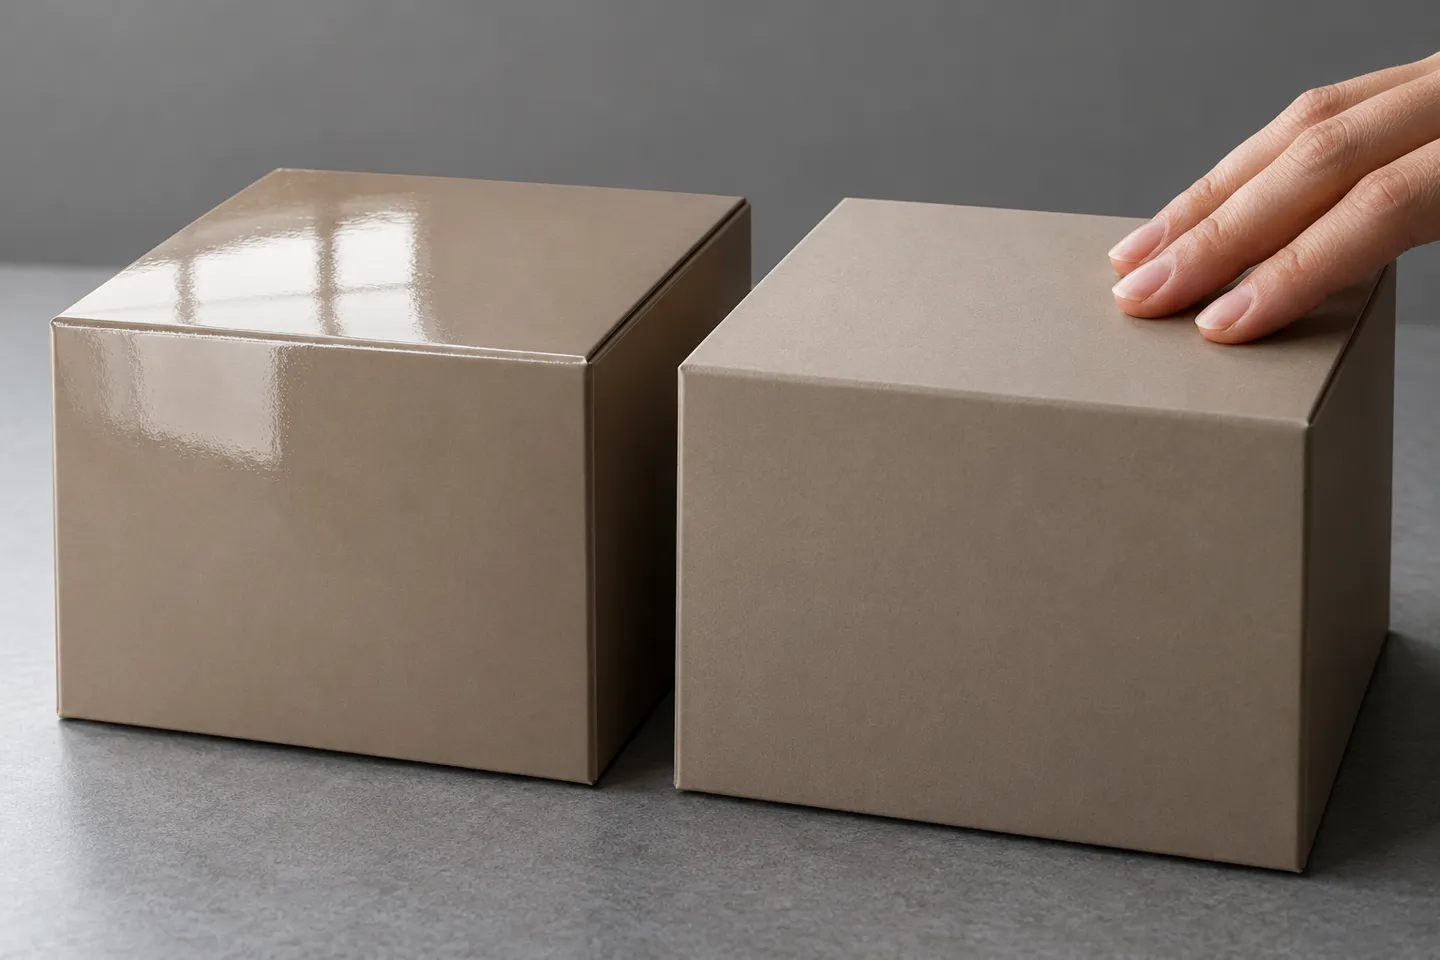
That film is BOPP, and the step is BOPP lamination. The laminate layer does three quiet jobs at once. It makes ink colors look deeper, it shields the print from moisture and scuffing, and it adds stiffness so cartons, bags and pouches survive handling. BOPP is the most common film for this job because stretching polypropylene in two directions gives it unusual clarity and strength for its thickness.
One boundary before we go further. This article is about laminating film onto print and packaging substrates in a production setting. It is not about the desktop pouch machine that seals an ID card, and it is not about the production lines that make BOPP film in the first place. If you specify packaging, run a print shop, or plan to buy laminating equipment, the next six sections follow the chain you actually make decisions on. It runs from film to bonding method to machine, and ends at what the whole investment does to your cost sheet.
Film Choices: Gloss, Matte, Metallized and Beyond
The film itself is the first decision, and it is mostly a marketing one. Each BOPP variant changes how the package reads on a shelf.
| Finish | What it looks like | Typical applications | Selection note |
|---|---|---|---|
| Gloss BOPP | High shine, colors read stronger | FMCG food, retail cartons, promotional print | The safest default when shelf impact matters most |
| Matte BOPP | Soft, non-reflective, premium feel | Cosmetics, luxury boxes, premium food | Shows fewer glare issues under store lighting; watch for silvering on dark solids |
| Metallized BOPP | Metallic sheen | Confectionery, gift packaging | Higher film cost; strong light barrier as a side benefit |
| Anti-fog BOPP | Clear with condensation control | Refrigerated fresh food | Engineered for cold display cases, not general print work |
| Thermal BOPP (pre-coated) | Gloss or matte with a heat-activated adhesive layer already applied | Sheet-fed print, book covers, cartons | The film carries its own glue, which shapes the whole process choice below |
Cartons, labels, flexible pouches and bags all take BOPP lamination well, which is why the same film family shows up across food, cosmetics, and retail packaging. The finish you pick changes what the customer sees. What it does not change is how the film gets bonded, how fast the line runs, or what the bond costs per square meter. That is the process decision, and it is where the real money sits.
The Four Ways BOPP Bonds to a Substrate
Every BOPP lamination line answers the same question differently: where does the bonding force come from? There are four working answers in production today, and each one carries its own adhesive logistics, curing behavior, speed ceiling, and failure habits.
The four routes at a glance
Thermal lamination: the adhesive rides on the film
Thermal BOPP film arrives pre-coated with a low-melt adhesive, usually EVA. The laminator heats a chrome roller, the adhesive softens, and nip pressure completes the bond. No liquid adhesive is poured, mixed, or cleaned. The bond sets as soon as the web leaves the heated roller, so laminated sheets move straight to cutting, foiling, or embossing with no waiting. That instant cure is why thermal owns short runs, samples, and sheet-fed work where turnaround is the selling point. The trade-off sits in the speed math: the film needs contact time on the hot roller for the adhesive to activate, so thermal laminators top out well below wet-bonding lines. Run one too fast and the bond comes out patchy, usually visible as bubbles that appear only on faster sections of the run.
Solventless lamination: two-component glue, no oven
Solventless lines bond roll-to-roll with a two-component polyurethane adhesive that contains no solvent and needs no drying oven. A metering system applies a whisper-thin glue layer, and the nip joins film to substrate. Industry references put film-to-film work at roughly 1.3 to 2.5 g/m² depending on ink coverage (Enercon, n.d.). Because there is no carrier to evaporate, these lines run fast and use little energy per meter. The catch is curing: the bond is not final when the roll comes off the machine. Solventless laminates need cure time at room temperature, and full cure ranges from several hours up to about two days depending on the adhesive chemistry (Nobelus University, 2024). Nothing can be slit, pouch-made, or shipped until the roll is cured, which turns part of your warehouse into a chemistry timer.
Solvent-based dry lamination: the oven route
Dry-bond lines coat a solvent-bearing adhesive, run the web through a drying oven with temperature zones, then laminate under nip pressure while the substrate is hot. The oven, commonly running around 80°C on production machines, evaporates the carrier and leaves the active adhesive behind. This route buys you aggressive bonds on difficult structures: paper to film, film to aluminum foil, retort-grade work. You pay for it in energy, in extraction, and in solvent handling. A dry line also occupies more floor length than a solventless machine of the same width, because the oven is simply long. Where substrates refuse to bond any other way, this remains the dependable answer.
Extrusion lamination: molten resin as the glue layer
Extrusion lines skip adhesives entirely. The machine melts resin, typically LDPE, PP, EVA or EAA, and extrudes it as a thin molten layer between the two substrates; the resin itself is the bond. Film gauges on these lines run from about 0.01 to 0.11 mm, and the process handles combinations adhesive systems struggle with: paper, textile fabric, nonwoven, knitted mesh. It is the standard route for functional structures rather than print protection, which is why it lives in food and medical packaging converting. Think of it as the fourth answer for the specific case where one of your layers is not a printable film at all.
A fifth, niche answer exists: adhesive-free thermal films that bond to themselves without any added glue. They serve luxury box and cover work where even minimal adhesive is unwanted, and for most converters they are a film purchase rather than a machine decision.
The curing difference is the one buyers underestimate most:
Curing reality check: thermal bonds are final the moment the sheet leaves the roller. Solventless bonds need several hours to two days of cure before the roll can be slit or converted. Dry-bond lines laminate immediately after the oven but carry oven energy and solvent handling instead. Plan floor space and work-in-progress around whichever timer your process uses.
Matching the Process to Your Order Book
None of the four routes is best in any absolute sense. The workable question is which failures and costs your specific order book can absorb. Three attributes of your orders decide it.
- Substrate structure. Film-to-film and film-to-foil roll work points to solventless. Paper-heavy premium structures point to dry bonding or thermal sheets. Nonwoven and fabric layers point to extrusion.
- Batch size and changeover frequency. Long runs reward the higher speed ceiling of solventless lines. Frequent short jobs punish any line with adhesive cleanup and curing waits, and favor thermal.
- Delivery promise. If you sell on turnaround, instant-cure thermal removes the biggest hidden wait. If you sell on unit price at volume, the cure timer matters less than meters per minute.
Run your last three months of orders through that filter and one route usually separates from the others:
Process self-check
- What substrate pairs dominate your orders, film/film, paper/film, or functional structures?
- What is your median batch length and how often do you change over?
- Do customers buy your speed or your unit price?
- Do you have floor space for a curing area, or floor length for an oven?
- Does your electrical supply support a multi-kilowatt oven line?
The industry direction adds context. Most modern flexible packaging converters prefer solventless adhesives, industry observers note (Nobelus University, 2024). The reasons are running cost, easier handling, and safety for workers and the environment. Low-VOC expectations keep pushing in the same direction. Treat the marketing claims with care, though. Thermal film sellers lead with “no adhesive at all”, and solventless sellers lead with “no solvent, minimal glue”. Both describe the same regulatory pressure from opposite sides. The question that actually matters for your customers is whether the finished structure, film plus substrate plus ink, meets the recyclability rules of the markets you sell into. One more case deserves a sentence. Digital print converters laminate near-line rather than inline, which leaves them free to pick any of the four routes based on order economics alone.
How to Read a Laminating Machine Spec Sheet
Once a route is settled, the purchase turns into a spec-sheet exercise, and spec sheets are written to look better than machines run. Two habits protect your budget: reading every number with its qualifier, and putting the qualifiers into the acceptance sheet before you sign.
The Two Speeds on Every Spec Sheet
Roll-to-roll laminators list two speed figures, and they are not synonyms. Mechanical speed is what the drive train can do with the machine running empty or near-empty. Laminating speed is what the machine sustains while actually bonding your structure, and it is always the lower number. On current production spec sheets the laminating figure commonly sits ten to twenty percent below the mechanical figure. A line advertised at 450 m/min mechanical typically laminates at 400 m/min; a 250 m/min dry-bond machine typically bonds at 220 m/min. The gap sounds small until you price a long run by the hour. Plan capacity on the laminating figure and treat the mechanical figure as a ceiling you will meet only in demos.
Acceptance criteria
Write this into your acceptance criteria: capacity is calculated on laminating speed at your coat weight and substrate, not on mechanical speed.
The sample book’s highest number is the mechanical rating.
What Else Belongs in the Acceptance Sheet
Web width comes first because it caps everything else. Production roll-to-roll lines cluster around 1050, 1250 and 1350 mm. Buy the width that covers your widest regular substrate, and resist paying for occasional oversize work that a partner plant could run.
Tension control is the item defect investigations keep circling back to. Independent tension control on unwind, laminate, and rewind motors keeps both webs moving at matched speeds through the nip. Four motors is the floor, eight on wider or faster lines. When a salesman cannot explain how many tension zones the machine has, that is the answer.
Adhesive metering decides your cost per square meter on every solventless meter you run. Ask what coat-weight range the metering system holds and how it is verified. On dry-bond lines, ask how many temperature zones the oven has and how each is controlled. Then look at total power honestly. Laminating lines range from tens of kilowatts for compact solventless machines up to 150 kW and beyond for wide dry-bond lines. Your building’s supply is part of the purchase price. Unwind and rewind roll diameters, commonly 600 to 800 mm, decide how often the line stops for splices.
The boundary matrix below condenses the whole decision:
Bonding route vs order reality
| Route | Order structure fit | Sweet spot | Switch away when |
|---|---|---|---|
| Thermal (pre-coated film) | Short runs, samples, sheet-fed cartons and covers | Instant cure, zero adhesive handling, fast turnaround | Long film/film runs at volume, where the thermal speed ceiling idles capacity |
| Solventless | Film/film and film/foil roll work, mid to high volume | Lowest glue cost per square meter, highest sustained laminating speeds, no oven energy | Paper-heavy or ultra-demanding structures needing more than 2-3 g/m² of adhesive |
| Solvent-based dry | Paper to film, film to foil, retort-grade demanding bonds | Strongest bonds on hard-to-bond structures | Energy budget, solvent handling, or floor length is constrained |
| Extrusion | Paper, nonwoven and fabric functional structures | Resin doubles as the bond layer; suits food and medical converting | Thin film/film print protection, where extruder setup overhead buys nothing |
When Lamination Goes Wrong: Defects and Their Machine-Side Roots
Defects are where process knowledge pays for itself, because almost every recurring lamination problem traces back to four root causes: film tension, nip pressure, temperature, and cure. The failures forum threads document look dramatic, but the causes are ordinary. One sign maker laminating motocross graphics reported a run that started clean for 30 centimeters, then produced a line of bubbles every 5 to 10 centimeters (Signs101 forum, 2023). The pattern repeated for the rest of the web. The community diagnosis came down to over-tight supply tension and excessive nip pressure deforming the roller, letting the two webs advance at slightly different rates. Trade press troubleshooting reaches the same trio from the other direction (PostPress, 2015). Insufficient supply tension traps air. Feeding faster than the laminator runs traps air. And laminating inkjet prints before the ink is dry puts bubbles over the heat spots that develop on idle rollers.
| Defect | First thing to check | Machine capability that prevents it |
|---|---|---|
| Bubbles | Supply roll tension, then nip pressure | Multi-zone tension control; even, adjustable nip |
| Wrinkles | Tension balance across the web width | Web guiding; roller condition |
| Curl | Tension balance between film and substrate | Symmetric tension zones; matched materials |
| Delamination | Coat weight and cure time | Accurate adhesive metering; a curing plan that is actually followed |
| Silver streaks | Nip roller surface condition | Roller maintenance schedule |
That table is a diagnostic order, not a checklist to clear in one pass. Work top to bottom, one change per shift, and write down what moved.
Change one variable at a time. A defect with four candidate causes becomes untraceable if you adjust tension, temperature, and speed in the same shift. And after any film or substrate change, previous settings are suggestions, not facts: run a short trial web first.
That trial habit scales up to the purchase itself. The most dependable acceptance test for a new laminator is running it on your own substrate, your own film, at your target coat weight, before the balance of payment moves. Machine makers who offer a pre-shipment trial on customer material, with video or a live witness, are easy to distinguish from those who do not.
The Business Side: Capacity, Curing and Cash
Read back through this chain and the investment math writes itself. Curing is working capital. Every solventless roll sitting in the cure room for one to two days is material, ink, machine time, and floor space that cannot be invoiced yet. And the cure room has to exist somewhere in a building you already think is full. Thermal lines skip that timer entirely, which is why a converter selling on turnaround can price jobs a wet line cannot. Speed ratings are unit cost. A long run priced on a mechanical 450 m/min and produced at a laminating 400 m/min delivers about eleven percent less capacity than the spreadsheet promised. That gap repeats every hour the job runs. Power is a fixed cost that arrives before the first meter is sold. And process mix is capacity strategy. A converter whose order book mixes long film/film runs with occasional premium paper work rarely fits one machine to both. The common shape is a solventless line as the volume engine and a thermal machine as the short-run sampler.
When you shortlist suppliers, five questions cut through the brochure. Which substrates can the line actually laminate? What does it sustain at your coat weight? How are the tension zones arranged? What is the acceptance test? And what must your electrical supply deliver? KETE’s laminating machine range, for example, publishes both speed figures on every model and lists web widths at 1050, 1250 and 1350 mm (laminating machine range). The series spans solventless two- and three-ply lines at 450 m/min mechanical and 400 m/min laminating. Dry-bond machines run from 150 to 250 m/min, and a 150 m/min extrusion line covers nonwoven and functional structures. Whatever brand you brief, hold the conversation to those five questions and the numbers on your acceptance sheet will match the numbers on your invoice.
If you want a second opinion on any of these parameters, we run prospective machines on your own material before shipment and back every unit with a warranty of at least one year, extendable to two on select models (pre-shipment trial runs).
Book Your Pre-Shipment Trial
Bring your film, substrate and coat weight. We run the machine on your own material before shipment, and the numbers on your acceptance sheet are the ones we sign against.
Schedule a Trial RunReferences
- Nobelus University. “How to Set Up Your Ideal Flex Pack Line: Choosing a Lamination Method.” 2024. nobelusuniversity.com
- Enercon. “Best Practices & Developments in Solventless Laminating.” n.d. enerconind.com
- PostPress. “Q&A: Common Issues in Laminating.” 2015. postpressmag.com
- Signs101.com. “Laminating Bubble Issue.” 2023. signs101.com