 EN
 RU
 ES
 FR
 AR
 PT
 IT
 ID
 KO
 TR
 DE
 VN
 TH
 IN
 JA
 ZH
 MS

A bottle of red arrives at the table with a colored sleeve around its neck. The server cuts a thin band just below the second lip, then peels the sleeve away in one piece. That sleeve is the capsule, the covering that sits over the cork and the top of the neck. One clarification about the word: this article is about that bottle-neck covering, not supplement capsules or coffee capsules.
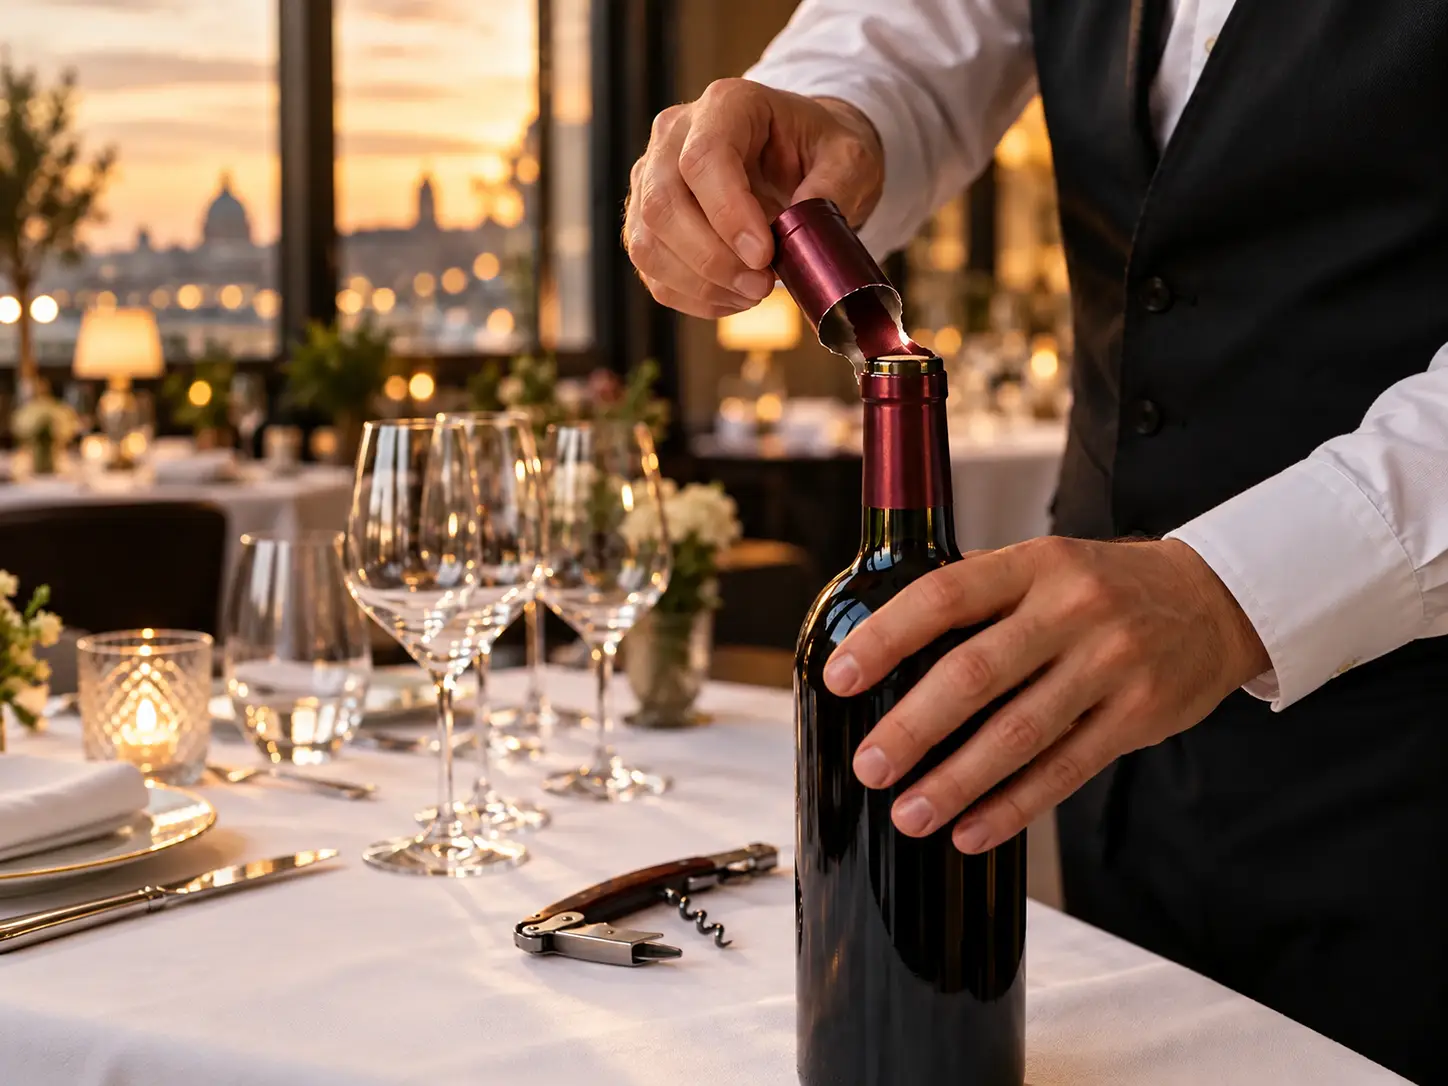
The capsule started life as pest control. Cellared wine once spent years in places where rodents and the cork weevil could attack an exposed cork, so a foil wrapper kept the stopper intact (Wikipedia, 2026). The collar also catches the first drips when you pour, which is why the cut line matters to anyone serving wine.
What the capsule does not do is change the wine. Once the cork is in, the foil adds nothing to the glass, and removing it entirely does no harm. Its modern job is closer to packaging than to preservation. It signals that the bottle has not been opened since it left the winery, and it carries the estate’s colors and crest. In France it can even be a legal requirement, since wines sold on the French domestic market must carry the CRD tax capsule (Wikipedia FR, 2026).
The material has a history worth knowing, because it explains what shelves hold today. Foils were once made of lead, until research showed that toxic traces could remain on the bottle lip and mix with the poured wine. Lead was phased out through the 1990s. In the United States, the FDA banned lead foils on domestic and imported wine bottles as of 1996 (Wikipedia, 2026). Tin, aluminium, heat-shrink plastic and laminates replaced it.
The Two Families of Wine Capsules: Shrink Sleeves and Preformed Shells
Every capsule on a shelf belongs to one of two families, and the family determines how the capsule behaves in your hand. The first and most common family is the shrink sleeve: a tube of PVC or PET-G film that slips loosely over the neck, then shrinks tight when heated. Home winemakers pull it on and hit it with a heat gun; a bottling line runs it through a shrinking tunnel or a spinner. The second family is the preformed shell, made of polylaminate, tin or aluminium and rolled into a fixed, seam-crimped shape at the factory. A shell never changes shape. It slides on and rolls tight, the way a tin cap fits a jam jar. Wax, poured over the cork, is a neighboring approach that skips both families entirely.
| Family | Structure | How it opens | Typical materials |
|---|---|---|---|
| Shrink sleeve | Loose tube, heat-shrinks to the neck | Tear-off tab, or a knife cut below the second lip | PVC, PET-G |
| Preformed shell | Factory-crimped, fixed shape | Knife cut; no shrink step | Polylaminate, tin, aluminium |
Both families can carry easy-open features, but they fail differently, and the failures come straight from the structure. On shrink sleeves, a weak tear-off tab leaves half the capsule stuck to the bottle. Wine professionals complain about exactly that (Reddit r/wine, 2023). Shrink quality is its own topic. Uneven hand heat leaves wrinkles, and one home winemaker put it plainly: “my labels are turning out great, but my capsules wrinkle. I use a heat gun” (WinemakingTalk, 2012). Shells avoid the heat problem but cannot shrink to hide an odd neck shape.
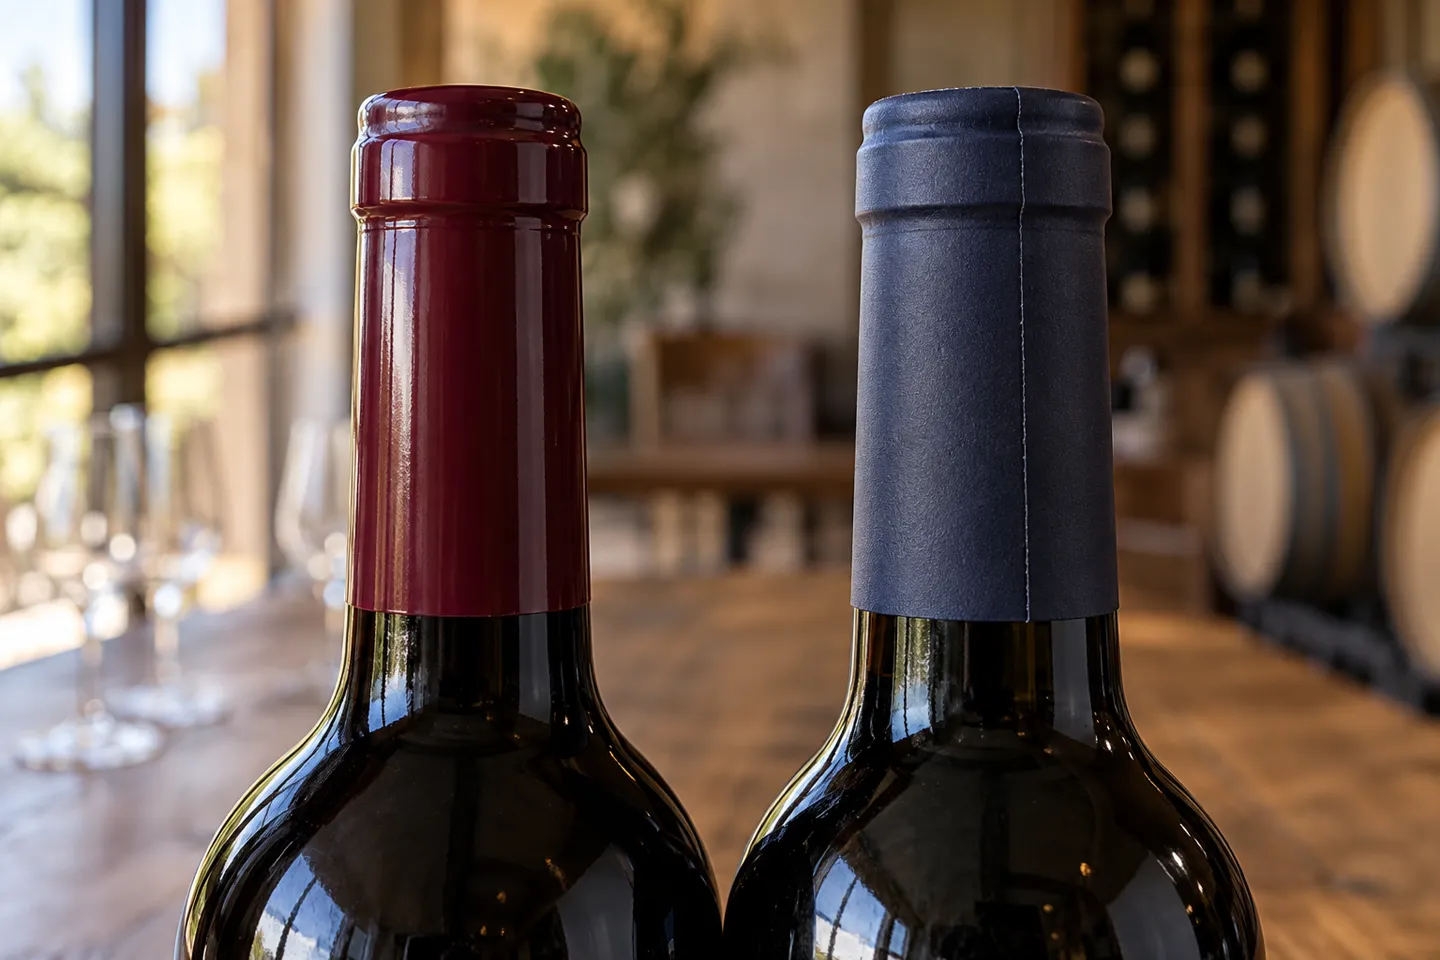
Age changes the picture in one specific way. On bottles twenty years old or more, the foil often bonds to the glass, so the whole capsule should come off before opening (Reddit r/wine, 2016). Sommeliers cut below the second lip, at the drip ring, for a clean pour and an intact label look.
Aged bottles: full peel before opening
Two decades in the cellar can fuse foil to the glass. Take the entire capsule off before the corkscrew goes in; a partial peel is for young wine.
The same shrink technology that dresses a wine bottle also seals other necks. Heat-shrink capsules close spice jars, five-gallon water bottles and gas cylinders. That same technology explains what a capsule factory can sell well beyond wine.
Do You Need a Capsule at All: The Debate, the Rules, and Your Three Ways to Get One
Wine media has been blunt about capsules lately. Wine Enthusiast ran a piece titled “Wine Capsules Have Got to Go,” arguing they serve no purpose (Wine Enthusiast, 2022). The Washington Post called bottle foil wasteful and annoying, and reported wineries dropping it entirely (The Washington Post, 2022). The criticism has real weight. Capsules cost money, they add a plastic or aluminum layer to a package that sells itself on minimalism, and they annoy servers when tabs tear.
Yet the market splits instead of disappearing. French domestic wine cannot legally ship without the CRD capsule, so that demand is fixed by law (Wikipedia FR, 2026). Sparkling wine needs a capsule with a formed top that no bare-cork presentation replaces. Tamper evidence still matters at retail. And at premium price points the capsule is brand canvas: colors, crest, texture, the tactile cue that this bottle is a gift. The estates abandoning capsules sit mostly in the everyday segment. The top of the market and the legal segment are not following.
What pushes capsules out
- Sustainability pressure and plastic fatigue
- Cost per bottle at volume
- Server frustration with torn tabs
- Minimalist glass-first presentation
What keeps capsules in
- CRD tax capsules required on French domestic wines
- Tamper evidence at retail
- Champagne and sparkling top forming
- Brand canvas and gifting cues at premium price points
If you do want capsules, there are exactly three ways to get them, and volume picks the door. Stock capsules from winemaking and packaging suppliers ship by the case, ready to apply with a heat gun or a small shrinking machine. That is how home winemakers and very small estates buy (Winemaking Superstore, 2026). Custom printed capsules add your artwork, and the supplier sets minimum order quantities per design and size, so the quote depends on your label count and colors. The third door is making capsules yourself. That is a production decision with its own economics, and the next two sections walk through what it actually requires.
Specifying a Capsule: Materials, Limits, and What to Ask For
Material by Material: What Each Type Actually Delivers
Choosing a capsule material is choosing a whole behavior, not a color. PVC shrink sleeves are the volume choice. They cost the least, shrink tight and glossy at modest temperatures, and dominate retail packs. Their weakness is reputational, since PVC carries the environmental baggage that feeds the anti-capsule argument. PET-G sleeves shrink with similar behavior and are the direction the market points when sustainability enters the spec, at a modest premium. Polylaminate shells are layers of aluminium with paper or film laminated in. They give the matte, substantial hand-feel that premium still wines and most champagne houses use, and they print beautifully because gravure-printed paper is part of the laminate. Tin shells sit at the top for ceremony and cost. Wax gets poured over the cork for the same visual effect at any budget.
Whichever material wins your spec, the line that runs it decides what the capsule costs at volume.
Match a line to your materialOne historical note belongs in any spec conversation. Lead is gone, banned in the US as of 1996 (Wikipedia, 2026). Talk of “tin feel” today means tin or aluminium, not the metal that used to be there.
Where Capsules Fail: Scenarios and Boundaries
Every capsule choice holds inside a boundary and fails outside one. The failures repeat so reliably that they can be tabulated. The table below is that working version: scenario by scenario, the option that fits, where it breaks, and the check that catches it before you order.
Capsule choice by scenario: fit, limits, and what to check
| Scenario | Better-fit option | Where it breaks | Check before ordering |
|---|---|---|---|
| Home winemaking, small batches | PVC shrink sleeve with hand heat | Heat gun wrinkles unevenly, gold foil worst | Vent holes present, 30 or 33 mm fit, test a dozen before a case lot |
| Estate bottling line | Shrink sleeve with machine application (spinner or tunnel) | Uneven heat shows as wrinkles at the bottom edge | Match tunnel temperature and conveyor speed to the film type |
| Sparkling and champagne | Polylaminate shell with formed top | Shrink film cannot form a mushroom top | Confirm top-forming tooling and neck diameter |
| Library stock and aged releases | Loose-fit shell or full-removal design | Old foil bonds to neck glass | Specify full-removal opening for older bottles |
| Bulk water, gas cylinders, spice jars | Heavy-gauge PVC or PET-G sleeve | Wine-grade film gauges do not fit industrial necks | Spec the actual neck diameter, not a wine standard |
| Hot climates and long sea transport | PET-G sleeve or polylaminate shell | Low-grade PVC turns brittle in heat cycles | Ask for temperature-cycle test data |
Read the matrix as actions, not judgments. “Test a dozen before a case lot” catches a bad film batch for the price of one bottle. “Match tunnel temperature to film type” separates a machine-made shrink from a hand-crumpled one. The film shrinks in a narrow temperature window, and every heat source behaves differently around it.
What to Ask a Capsule Supplier Before You Order
The questions that separate a real capsule supplier from a reseller are specific. Ask for food-contact documentation under the rules that apply in your market, since the capsule touches the pour point of the bottle. Ask for the shrink temperature range of the film and the heat source the supplier recommends, then check both against the equipment on your bottling line. Ask for a neck-fit table matching capsule diameter to your bottle’s finish; most cork-finish bottles take 30 or 33 mm, but your bottle, not the category, decides. On custom print, ask what the plate costs, what the minimum order per design runs, and what the lead time looks like at your seasonal peak. Ask, finally, which easy-open features are standard and which are options: tear-off tabs, vent holes, perforation, embossing. A supplier who answers those five questions with numbers is a supplier you can hold to numbers.
The capsule RFQ checklist
- Food-contact paperwork for your market; the capsule sits at the pour point.
- Shrink temperature range and the recommended heat source, matched to your bottling line.
- Neck-fit table: capsule diameter vs. bottle finish; 30 or 33 mm is typical, and your bottle decides.
- Custom print economics: plate cost, minimum order per design, lead time at your seasonal peak.
- Easy-open options: tear-off tabs, vent holes, perforation, embossing, standard vs. optional.
From Buying Capsules to Making Them: What a Capsule Line Really Takes
When Making Your Own Capsules Pays (and When It Doesn’t)
Buying capsules forever and making them in-house are both rational, and the boundary between them is measurable. In-house production starts to pay when monthly consumption climbs far past the minimum orders custom suppliers set. At that volume you are buying PVC or polylaminate by the ton and converting it yourself for pennies of material per capsule. It pays better when changeovers matter. An estate that reprints artwork every vintage, or a converter serving dozens of wineries, values a line in the building more than a supplier’s queue. It does not pay when one customer controls the volume, when the order book is seasonal, or when the plant would sit idle between peaks. A capsule line is an asset that wants feeding. The honest make-or-buy test is whether your demand, across materials and neck sizes, runs steady enough to keep it fed.
The Production Chain Behind Every Capsule
A capsule is a printed, cut and formed product, and the line mirrors that order. Sleeve forming starts the chain: pre-cut PVC or PET-G film is seamed into tube at around 250 m/min class. Gravure printing lays down the artwork on the film or the laminate at 150 to 180 m/min class, which is why capsule print has that solid, catalog-crisp look. Slitting cuts the printed web to capsule width at 400 to 600 m/min class. The cutting station then chops sleeves to capsule length at up to 500 cuts per minute class. Forming is the last conversion step. A standard PVC or polylaminate line forms 160 capsules per minute mechanical, a high-speed line 250, and a champagne line 130 with top forming.
Sleeve forming. Seaming, around 250 m/min class.
Gravure printing. 150 to 180 m/min class.
Slitting to width. 400 to 600 m/min class.
Cutting to length. Up to 500 cuts per minute class.
Capsule forming. 130 to 250 caps/min mechanical by line type.
Inline inspection with automatic rejection.
Auto counting and packing.
That sequence is easier to evaluate when you can see the material move through an actual production line. The video below shows a polylaminate wine capsule machine forming the capsule, adding the C-punch and tear line, and applying gold stamping at production speed.
A KETE polylaminate wine capsule machine demonstrates C-punching, tear-line forming and gold-stamping operations.
After these forming and decoration steps, the quality stage runs inline. Machine-vision inspection checks each capsule and automatically rejects defective ones before packing, while auto counting bundles the output into counted lots. On an inspected line, the reject never reaches the customer’s carton. On a manual line, someone counts and visually checks every capsule by hand at the end.
Nameplate Speed, Real Speed, and the Case for Automation
Every forming machine carries two speed figures, and the gap between them is where capacity plans go wrong. Published figures for current lines make the gap concrete. A standard PVC or polylaminate line nameplates 160 capsules per minute and lists a working speed of 120 to 150. A high-speed line nameplates 250 and works at 180 to 220. A champagne line nameplates 130 and works at 100 to 120 (wine capsule machine range, 2026).
Nameplate speed vs. working speed
Mechanical nameplate, then published working speed, capsules per minute.
Plan on the working speed and keep 20 to 30 percent in reserve for changeovers.
That reserve is not pessimism. It is where champagne tops, neck-size changes and artwork swaps actually land. Multiply the difference across a shift and the gap buys or costs a pallet of capsules. Automation is what narrows it. Inline inspection with automatic rejection means speed never has to drop for a quality check. Auto counting removes the manual pack-out that quietly caps a line’s real output. When you compare quotes, ask each machine maker for the working speed at your materials and neck sizes, not the nameplate. Then ask what a changeover between a flat top and a champagne top costs in minutes.
How to Read the Capsule Business Like an Operator
The trend headlines read like a shrinking market, but the operator’s ledger splits the category before it does any math. PVC shrink sleeves carry the everyday segment, where volume is high and the anti-capsule argument lands hardest. Polylaminate shells carry the premium and legal segments, where the CRD obligation and champagne top forming keep demand structural. A line configured for a single material is a bet that one column of that ledger never moves. The two columns have been moving in opposite directions since 2022.
The automation decision is where the margin actually gets made. Inspection, rejection and counting decide whether a plant sells machine hours or sells good capsules. A manually inspected line caps its output at the pace of the counting table. An inspected line keeps forming speed and loses only the rejects, automatically.
Capacity honesty is the last discipline. Working speed, not nameplate, is what a delivery promise is made of. The 20 to 30 percent reserve for changeovers is the difference between a line that hits its schedule and one that explains itself. Operators who quote on nameplate win the order and lose the shift.
This is the point where reading about capsules turns into running them. We build capsule lines at KETE. Our range covers PVC and PET-G shrink sleeves as well as Polylaminate shells, including champagne top formation. It pairs forming machines with sleeve seaming, gravure printing, slitting and cutting. The forming machines run at 160, 250 and 130 capsules per minute mechanical depending on the line, with inline inspection, automatic rejection and auto counting. The wine capsule machine range lists the figures used in this article. If you are weighing a line against your own capsule volumes, our engineers will size it to your real bottleneck rather than the nameplate.
Size a capsule line to your real bottleneck
KETE builds shrink-sleeve and shell capsule lines at 160, 250 and 130 capsules per minute, with inline inspection, automatic rejection and auto counting.
Get a line quoteReferences
- Wikipedia. “Wine Bottle.” Accessed 2026. wikipedia.org
- Wine Enthusiast. “Wine Capsules Have Got to Go.” 2022. wineenthusiast.com
- The Washington Post. “Wine Bottle Foil Is Wasteful, Annoying and Going Away.” 2022. washingtonpost.com
- Wikipédia. “Capsule représentative de droits.” Accessed 2026. wikipedia.org
- WinemakingTalk Forum. “Heat Shrink Capsules.” 2012. winemakingtalk.com
- Reddit, r/wine. “Wine Pros of Reddit, What Immediately Bothers You About Someone’s Wine Knowledge or Habits?” 2023. reddit.com
- Reddit, r/wine. “What Is the Correct Way to Remove a Foil Capsule?” 2016. reddit.com
- Winemaking Superstore. “Wine Bottle PVC Shrink Capsules.” Accessed 2026. winemakingsuperstore.com